Achieving 2 Million+ Cycles: The Role of S136 Steel, Vacuum Heat Treatment, and Precision Machining
Written by the Metallurgy & Tooling Engineering Team at ApexMolds — Experts in High-Durability PET & rPET Preform Mold Solutions.
1. Introduction: The Demand for Ultra-Long Tooling Lifespan
In high-volume PET container manufacturing, mold longevity directly determines production profitability and total cost of ownership (TCO). A high-cavity preform mold operating 24/7 undergoes millions of clamping, injection, and ejection cycles annually. Premature wear, corrosion from recycled resins (rPET), or micro-cracks can cause catastrophic flash, concentricity failures, and severe downtime.
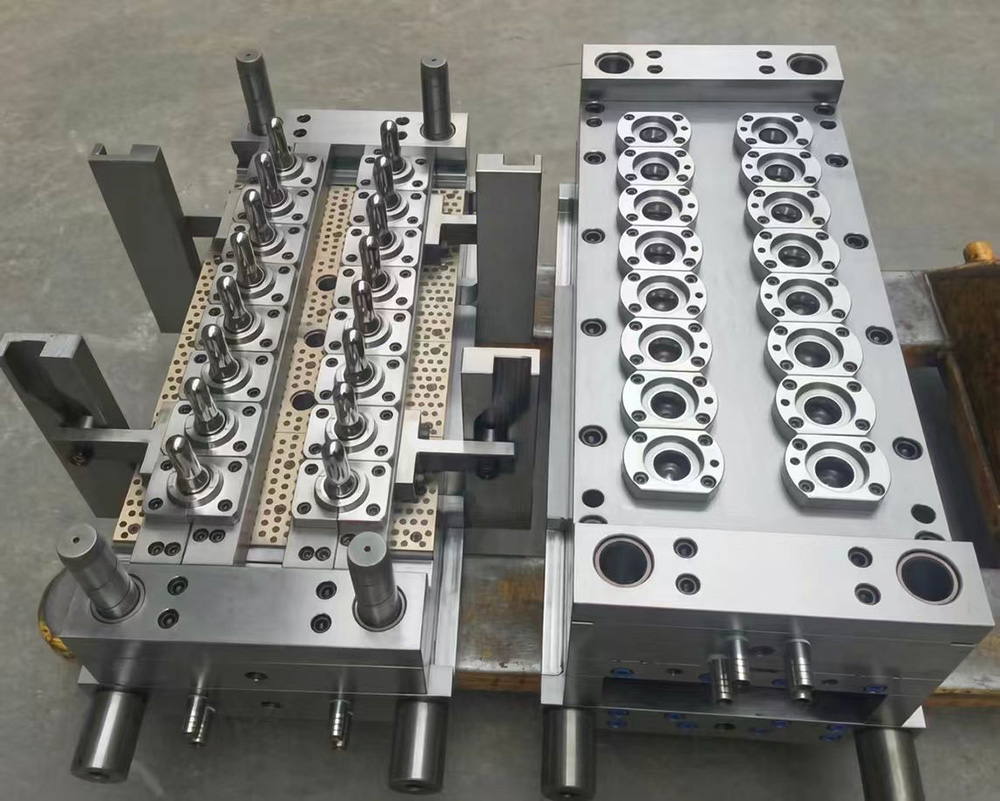
At ApexMolds, our high-cavity preform molds are engineered to achieve an exceptional service life exceeding 2 million+ cycles without compromising critical tolerances. This level of durability is made possible through a synergistic combination of premium S136 stainless steel, state-of-the-art vacuum heat treatment, and sub-micron precision CNC machining.
2. S136 Stainless Steel: The Superior Core and Cavity Material
Selecting the correct tool steel is the foundation of high-performance mold engineering. ApexMolds utilizes ESR (Electro-Slag Remelted) premium S136 stainless steel (equivalent to AISI 420 Stainless / DIN 1.2083) for all core, cavity, and neck ring inserts. S136 offers distinct material advantages:
- Exceptional Corrosion Resistance: Prevents pitting caused by volatile off-gassing during PET/rPET melting and humid ambient cooling environments.
- High Mirror-Polishing Capability: Achieves an ultra-smooth surface finish (SPI A1 standard), ensuring easy preform ejection and superior optical clarity.
- High Wear Resistance: Resists abrasive wear at parting lines, neck threads, and gate areas caused by continuous friction and high clamping forces.
3. Vacuum Heat Treatment: Unlocking Optimal Metallurgy
Raw S136 steel alone is insufficient without controlled thermal processing. ApexMolds subjects all core and cavity inserts to multi-stage vacuum heat treatment followed by cryogenic treatment to optimize the microstructure:
A. Controlled Hardening and Tempering
By heating steel in a high-vacuum furnace, surface oxidation and decarburization are completely eliminated. The components are hardened to 48–52 HRC, striking the ideal balance between structural toughness and wear hardness.
B. Cryogenic Deep Freezing
Sub-zero cryogenic treatment converts retained austenite into martensite within the steel structure. This process eliminates internal stresses, guarantees dimensional stability over millions of thermal expansion cycles, and prevents micro-deformation during operation.
4. Sub-Micron Precision Machining and Alignment
Even the hardest steel requires extreme geometric accuracy to operate smoothly across 48, 72, or 96 cavities. ApexMolds leverages advanced 5-axis high-speed CNC machining, optical profile grinding, and EDM to achieve strict tolerances:
| Tooling Parameter | ApexMolds Standard | Impact on Preform Quality & Lifespan |
|---|---|---|
| Concentricity Tolerance | $\le 0.005 \text{ mm}$ | Prevents uneven wall thickness and eliminates core deflection fatigue. |
| Parting Line Alignment | Sub-micron positioning | Eliminates parting line flash and reduces local clamping wear. |
| Surface Roughness (Core) | $Ra < 0.05 \ \mu\text{m}$ | Ensures smooth robotic take-out and reduces ejection force requirements. |
5. The ApexMolds Advantage: 2 Million+ Cycles Guaranteed
By controlling every phase—from raw ESR S136 steel verification to cryogenic vacuum heat treatment and precision grinding—ApexMolds delivers preform molds that set industry standards for longevity and precision. Whether processing virgin PET or aggressive 100% rPET, our tools minimize maintenance cycles and lower long-term unit production costs.
Ready to upgrade your bottling lines with durable, ultra-precise preform tooling? Contact the mold specialists at ApexMolds today to discuss your custom project requirements.