Preform Mold and Closure Mold Integration: Ensuring Perfect Neck Finish Compatibility
Written by the Precision Tooling & Packaging Systems Team at ApexMolds — Global Experts in High-Cavity PET Preform & Neck Finish Tooling Solutions.
1. Introduction: The Critical Interface of PET Bottle Systems
In high-speed rigid packaging lines for carbonated soft drinks (CSD), mineral water, dairy, and hot-fill beverages, the interface between the bottle neck finish and the plastic closure is the single most sensitive point of failure. A misalignment of even 0.02 mm in thread geometry, pitch diameter, or sealing lip compression can result in catastrophic product leaks, rapid loss of carbonation, or cap cross-threading during high-speed capping.
Traditionally, brand owners and converter plants souring preform molds and closure molds from separate vendors face expensive integration friction, dimensional discrepancies, and prolonged troubleshooting during line commissioning. At ApexMolds, we address this industry bottleneck through total system integration engineering. By co-designing and co-manufacturing preform mold neck finish stacks in tight alignment with closure mold specifications, ApexMolds delivers turn-key seal integrity, smooth torque performance, and zero-defect high-volume production.
2. Key Technical Challenges in Neck Finish & Closure Engineering
Achieving perfect physical, mechanical, and functional harmonization between the preform neck finish and the molded closure requires overcoming complex thermodynamic and mechanical hurdles:
| Technical Parameter | Dimensional Challenge | Engineering Impact on Package Performance |
|---|---|---|
| Sealing Lip & Plug Fit | Inward or outward sink marks on the E-lip/bore seal area. | Loss of pressure tightness, CO₂ leakage in CSD, or micro-bacterial contamination in sensitive juices. |
| Thread Profile & Pitch Angle | Non-uniform contact stress along the thread flank. | High capping torque requirement, cap back-off during transportation, or thread stripping. |
| Tamper-Evident (TE) Band Engagement | Improper retaining bead clearance or sharp edge radius. | Premature TE ring bridge breakage during capping or failure to break upon initial opening. |
| Material-Specific Volumetric Shrinkage | PET vs. HDPE/PP differential contraction during cooling. | Post-mold warping and ovality leading to inconsistent sealing tightness across high-cavity layouts. |
3. ApexMolds Integrated Engineering Protocols
ApexMolds employs a systemic, closed-loop design and manufacturing workflow that aligns preform tooling with cap tooling parameters from concept to final sampling:
A. Co-Optimized Thread Profile CAD/CAM Modeling
Whether manufacturing standard neck finishes (such as PCO 1881, 26/22 lightweight finishes, 29/25 water finishes, 38mm 3-lead hot-fill) or customized proprietary geometries, ApexMolds utilizes joint 3D finite element analysis (FEA). We model the dynamic interaction between the rigid PET preform neck finish and the flexible HDPE/PP closure under clamping, gas pressure, and removal torque conditions before cutting steel.
B. Sub-Micron Precision Machining of Neck Ring Stacks
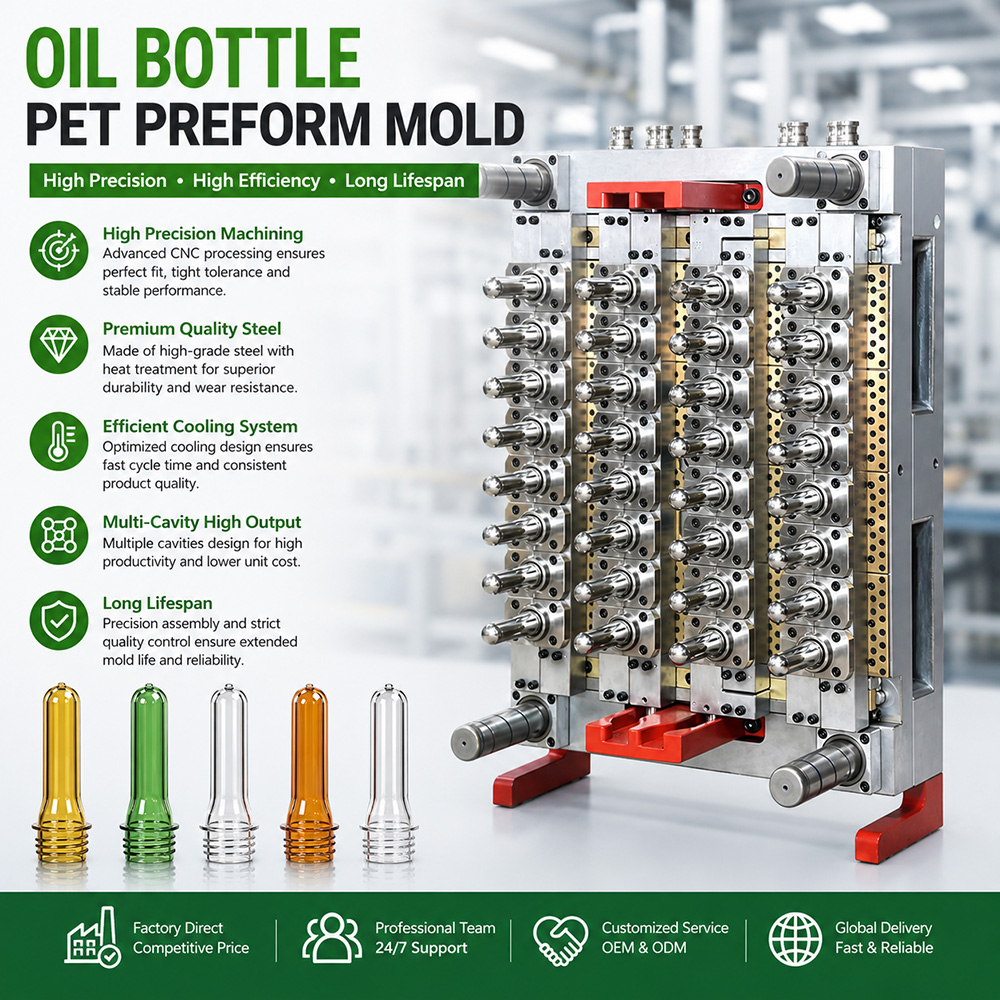
The neck split rings are the heart of the preform cavity stack. ApexMolds manufactures neck components using premium S136 ESR stainless steel hardened to 52-54 HRC. Utilizing multi-axis CNC jig grinding and high-speed EDM with sub-micron tolerances (< 2 μm), we eliminate parting line flash, ensure razor-sharp thread definitions, and guarantee perfect concentricity across 48, 72, 96, and 128 cavities.
C. Advanced Thermal & Shrinkage Compensation for rPET / Virgin Blends
Recycled PET (rPET) exhibits variable crystallization behavior and thermal expansion rates compared to virgin PET resin. ApexMolds incorporates proprietary cooling channel layouts direct-cooled right under the neck ring threads. This rapid, uniform cooling minimizes ovality and thermal distortion, preserving critical 'A' (thread outside diameter), 'E' (wall thread root diameter), and 'T' (thread diameter) dimensions regardless of resin IV fluctuations.
D. Turn-Key Leakage & Removal Torque Testing
Before mold delivery, ApexMolds conducts comprehensive integration testing using customer-specified cap designs. Tests include:
- Secure Seal Tester (SST): Pressurization up to 12+ bar to verify zero gas leakage.
- Automated Torque Analyzer: Ensuring opening torque remains within ergonomic standards (1.2 – 1.8 Nm) while maintaining secure sealing.
- Optical CMM 3D Profilometry: Verification of thread surface contact ratios and zero parting line flash.
4. Benefits of Partnering with ApexMolds for Integrated Tooling
Choosing an integrated neck-finish solution specialist delivers tangible operational advantages for bottle converters and beverage manufacturers:
- Accelerated Time-to-Market: Simultaneous preform and closure design validation reduces project lead times by 30-40%.
- Elimination of Inter-Supplier Disputes: Single-point accountability guarantees that preforms and caps fit flawlessly right from start-up.
- Lightweighting Optimization: Safely reduce material weight in the neck area by up to 1.5 grams without sacrificing cap retention or seal pressure.
- Extended Tooling Durability: Reduced mechanical wear on neck splits and capping heads due to precise thread alignment, enabling 2 Million+ cycles with low maintenance.
5. Conclusion: Achieve Perfect Packaging Integrity with ApexMolds
In high-speed beverage production, true efficiency relies on the precise fit between the preform neck finish and the closure. By choosing ApexMolds, you gain a dedicated partner capable of engineering high-cavity PET preform tooling and neck finish components designed for absolute compatibility, zero leaks, and smooth capping performance.
Looking to upgrade your production line or develop a lightweight neck finish? Contact ApexMolds engineering team today for expert consultation and customized tooling solutions.