Processing Up to 100% rPET in High-Cavity Preform Molds: Engineering Solutions for Material Variability
Written by the Engineering Team at ApexMolds — Global Leaders in High-Cavity PET & rPET Tooling Innovations.
1. The Shift Toward 100% rPET and the Manufacturing Challenge
As sustainability regulations tighten globally and circular economy initiatives gain traction, beverage brands are accelerating the transition from virgin PET to high-content recycled PET (rPET), up to 100%. While this transition reduces carbon footprint significantly, it introduces complex thermal and rheological challenges into high-cavity injection molding systems.
At ApexMolds, we specialize in overcoming these operational hurdles. Processing 100% rPET in 48-, 72-, or 96-cavity molds requires more than standard tooling—it demands advanced engineering designed specifically to handle material variability, Intrinsic Viscosity (IV) fluctuations, and thermal sensitivity.
2. Key Technical Challenges of 100% rPET Processing
Unlike virgin PET resin, recycled PET flakes and pellets present several inconsistent physical properties that disrupt standard injection molding workflows:
- Intrinsic Viscosity (IV) Fluctuation: Degraded molecular chains in rPET lead to IV drops, causing unpredictable melt viscosity and uneven cavity filling.
- Higher Thermal Sensitivity: Residual contaminants and recycled polymer blends melt at varying temperatures, increasing the risk of thermal degradation and AA (Acetaldehyde) generation.
- Melt Inconsistencies & Black Specks: Variations in material purity create pressure drops, gate stringing, and contamination clogging in standard hot runner nozzles.
- Increased Mold Wear: Recycled materials can exhibit higher abrasive characteristics, accelerating core and cavity wear if standard steel grades are used.
3. ApexMolds Technical Solutions for 100% rPET Performance
To enable seamless, high-speed production with 100% rPET, ApexMolds implements a multi-faceted technical architecture across hot runner design, metallurgy, and cooling engineering:
A. Rheologically Balanced Hot Runner Systems
To mitigate IV variations, our hot runner manifolds feature custom flow-channel geometry designed through computational fluid dynamics (CFD) simulation. Equal shear rate distribution across all channels ensures consistent pressure transfer, preventing short shots or flash in high-cavity setups (48, 72, and 96 cavities).
B. Advanced Valve Gate Technology & Anti-Clogging Nozzles
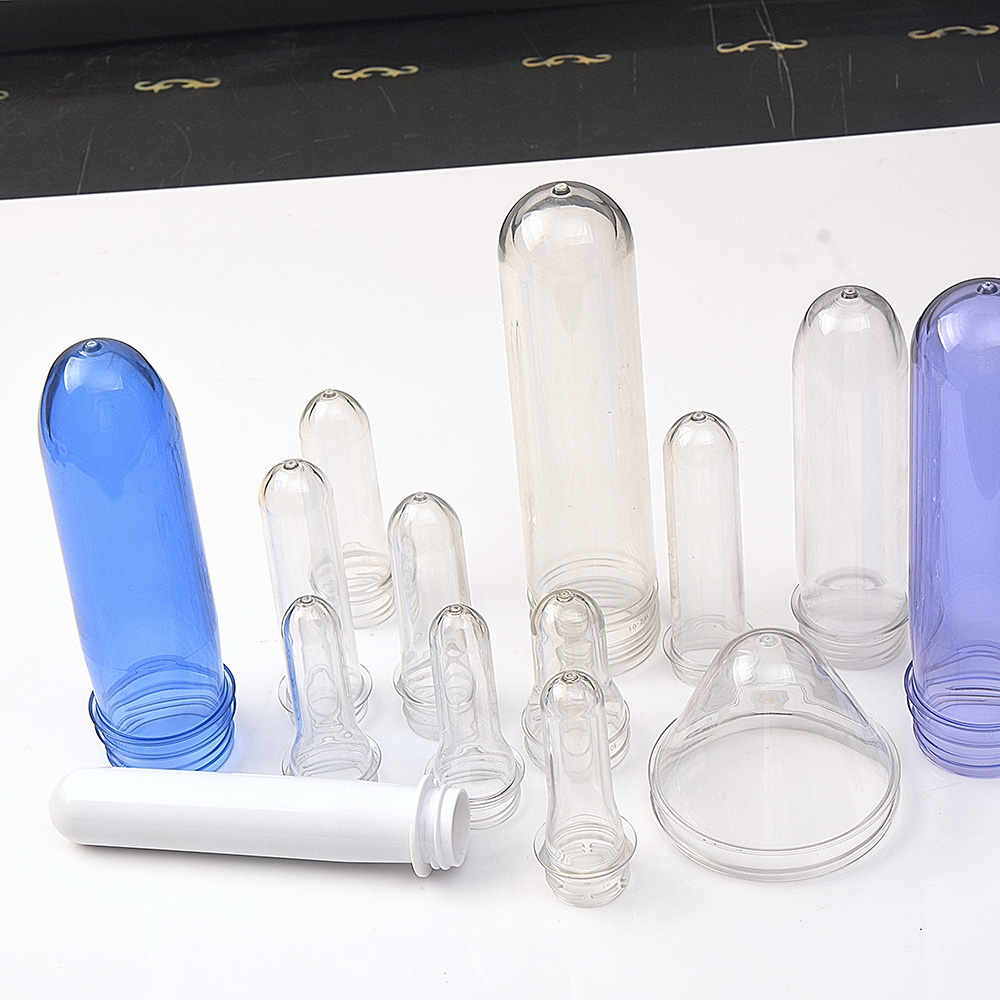
ApexMolds utilizes precision pneumatic/hydraulic valve gate systems with custom-engineered nozzle tips. The direct mechanical shut-off prevents gate drooling and stringing caused by lower IV rPET melts, producing clean, vestige-free preform gates ideal for automated down-stream handling.
C. Premium Metallurgy & Wear-Resistant Coatings
We craft our cavity and core components from high-hardness Swedish and German stainless steels (e.g., S136, 1.2083) enhanced with specialized physical vapor deposition (PVD) anti-wear coatings. This protects critical mold surfaces against abrasion from recycled contaminants, ensuring extended tool lifespan and micron-level dimensional stability.
D. Optimized Conformal Cooling Circuitry
rPET requires precise temperature management to prevent localized crystallization. ApexMolds integrates optimized cooling channels around the cavity neck finish and core body, maximizing heat extraction efficiency and shortening overall cycle times while maintaining crystal-clear optical clarity.
4. Quantifiable Benefits for High-Volume Packaging
By integrating ApexMolds' rPET-optimized tooling solutions, high-volume container manufacturers achieve superior operational resilience:
- Seamless Material Adaptability: Run 0% to 100% rPET blends without needing hardware modifications or extensive downtime.
- Consistent Preform Weight: Maintain strict weight tolerances within ±0.1g across all cavities, even with varying IV raw feeds.
- Optimal Cycle Speed: Achieve fast cycle times comparable to virgin PET molding.
- Reduced Total Cost of Ownership (TCO): Extended mold durability and lower scrap rates maximize production profitability and ROI.
5. Partner with ApexMolds for Sustainable Tooling Success
Transitioning to 100% rPET does not mean compromising on production efficiency or preform quality. With ApexMolds as your technical partner, you gain access to state-of-the-art mold design, robust metallurgy, and tailored hot runner solutions built for the future of sustainable packaging.
Ready to optimize your high-cavity lines for rPET? Contact ApexMolds engineers today for an in-depth technical consultation.