Wall Thickness Eccentricity Control: Achieving ≤0.10mm Over 100mm Length
An Advanced Technical Analysis of Core-Cavity Alignment, Thermal Expansion Balance, High-Precision Injection Tooling, and PET Preform Dimensional Stability
1. Introduction to PET Preform Eccentricity Challenges
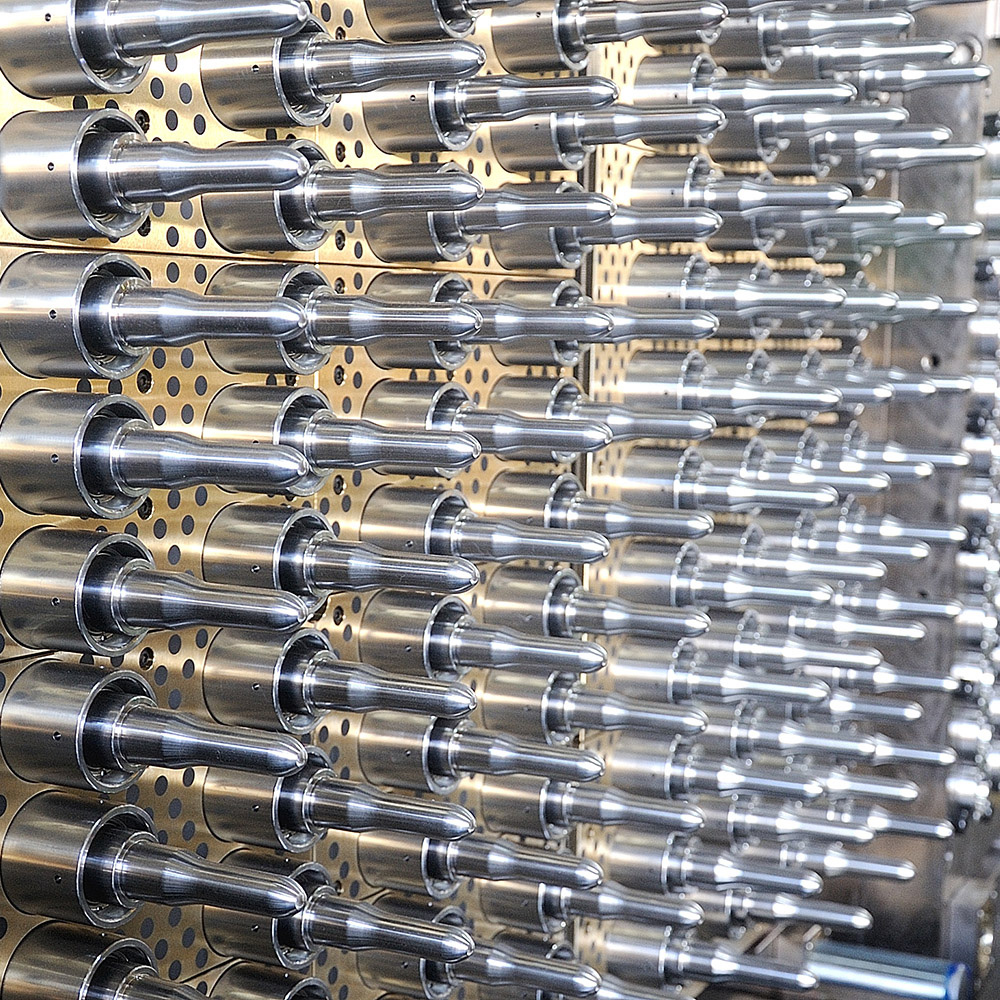
In high-speed PET stretch blow molding and packaging production, preform wall thickness eccentricity is a critical quality metric. Even minor wall thickness deviations across the body length result in asymmetrical container expansion, localized thinning, weakened top-load performance, and failed burst tests during subsequent blowing stages. Achieving a strict eccentricity tolerance of ≤0.10mm over a 100mm preform length demands exceptional mechanical rigidity, micro-toleranced machining, and advanced thermal management. As an industry-leading manufacturer specializing in high-performance preform molds, Apexmolds engineers cutting-edge tooling platforms designed to eliminate core shift and guarantee absolute wall thickness uniformity.
2. Root Causes of Wall Thickness Eccentricity in Injection Molds
1. Core Deflection Under High Injection Pressure
During the injection phase, molten PET resin enters the cavity under extreme pressures. Asymmetrical flow dynamics or insufficient core rigidity cause lateral deflection of the long slender core pins. This core shift directly results in uneven annular gaps between the core and cavity, creating localized thick and thin walls along the preform body.
2. Thermal Expansion Asymmetry and Cooling Imbalance
Uneven cooling channel layouts within the mold body lead to localized thermal gradients. Differential thermal expansion across mold plates causes minor misalignments between core inserts and cavity rings, compromising concentricity during high-temperature injection cycles.
3. Apexmolds Engineering Solutions for Precision Eccentricity Control
To consistently achieve wall thickness eccentricity of ≤0.10mm over 100mm length, Apexmolds integrates advanced mechanical and metallurgical features into every preform mold:
- High-Rigidity Core Pin Metallurgy: Utilizing premium pre-hardened stainless steel alloys with superior tensile strength and proprietary anti-deflection geometry, minimizing lateral core bending under peak injection pressures.
- Precision Interlock Taper Alignment: Designing robust conical self-aligning interlocks between core plates and cavity plates to lock components into absolute concentricity prior to melt injection.
- Conformal and Isothermal Cooling Circuits: Engineered cooling channels surrounding each cavity ensure uniform heat extraction, eliminating thermal distortion and maintaining tight dimensional stability.
4. Comparative Performance Matrix: Standard vs. Apexmolds Tooling
| Engineering Parameter | Conventional Preform Molds | Apexmolds High-Precision Tooling Solution |
|---|---|---|
| Wall Thickness Eccentricity | ±0.18mm to ±0.25mm over 100mm | ≤0.10mm over 100mm length precision |
| Core Deflection Resistance | Standard steel core susceptibility | High-rigidity alloy core with zero lateral shift |
| Thermal Stability | Variable cooling gradient across plates | Balanced isothermal cooling with zero thermal distortion |
| Preform Stretch Consistency | Asymmetrical blowing & thinning risks | Uniform biaxial orientation and flawless bottle strength |
5. Why Partner with Apexmolds
As a premier manufacturing enterprise specializing in high-performance PET preform molds, Apexmolds combines advanced CAD/CAM engineering, ultra-precision CNC machining, and rigorous quality control protocols. Whether you are producing lightweight water preforms, thick-walled cosmetic jars, or large-capacity container preforms, our custom tooling solutions ensure unmatched structural integrity, minimal scrap rates, and maximum production efficiency. Contact Apexmolds today to consult with our preform mold engineering specialists.